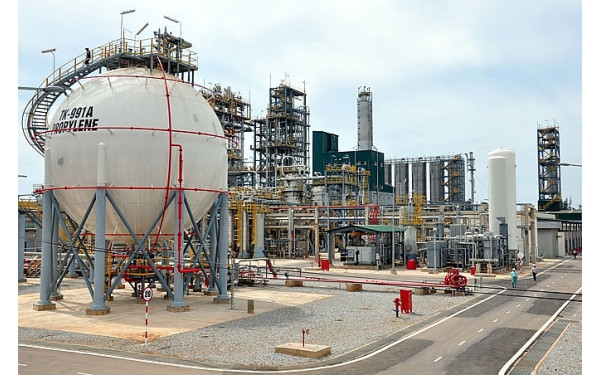
Mining operations face extreme fire risks from heavy mobile equipment, fuel storage, and increasingly, lithium-ion battery systems powering underground machinery. These high-hazard environments often combine combustible dust, hydraulic fluids, and confined spaces where fires can spread rapidly. Hazard Control Technology’s advanced fire suppression systems, powered by F-500 Encapsulator Agent, are engineered to protect workers, equipment, and production continuity in mining environments.
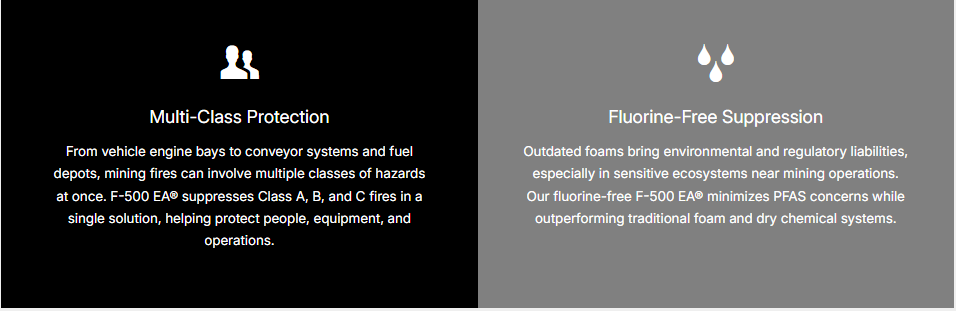
Unlike outdated foams, F-500 EA suppresses multiple fire classes, including Class A, Class B, electrical, and combustible metal hazards common in the mining sector. Specifically designed with mining safety in mind, F-500 EA® is MSHA-approved and trusted to protect crews and equipment in the most demanding underground and surface operations. By minimizing re-ignition, limiting equipment damage, and maintaining compliance with mining safety standards, F-500 EA® provides proven protection to keep operations safe and productive. Supported by more than fifteen years of NFPA-recognized third-party testing, it stands as a reliable choice for the mining industry.
Our fire protection solution mitigates unique fire risks underground. F-500 EA® addresses battery fires on three levels:
F-500 EA® absorbs heat and encapsulates electrolytes to halt thermal runaway.
F-500 EA® suppresses toxic and explosive off-gases before they accumulate in confined shafts.
F-500 EA® reduces carcinogens and smoke particulates, keeping air safer for miners and first responders.
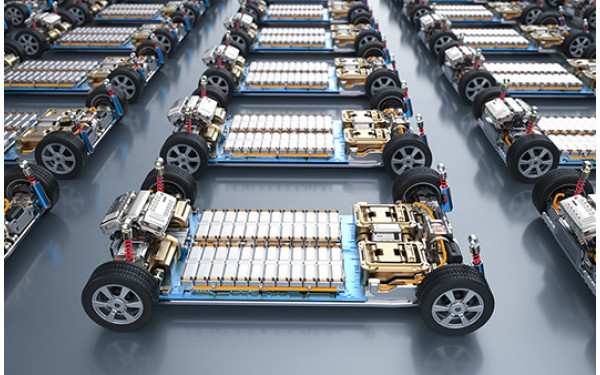
As the mining industry expands lithium production and adopts battery-powered machinery, fire risks increase across both electric and diesel-powered fleets. Lithium-ion batteries in heavy-duty mining vehicles, drills, and electrical components can fail under heavy loads, while diesel fuel fires in engine compartments remain a constant hazard. F-500 EA® suppresses by cooling heat sources, encapsulating fuels, and preventing re-ignition. From battery malfunctions to vehicle fire events, our systems deliver reliable protection to keep crews and equipment safe in demanding mining environments.

Coal dust is a persistent fire hazard in underground mining operations, especially in harsh conditions where fine particulates accumulate around equipment. F-500 EA® reduces combustible buildup and eliminates hot spots before ignition occurs. By integrating this solution into routine maintenance, mining facilities strengthen fire prevention, protect workers, and improve overall mine safety.

Mining companies require fire protection equipment that goes beyond traditional methods to address the hazards of underground and surface operations. Our fluorine-free systems deliver advanced fire safety by suppressing ignition risks, reducing toxic smoke, and protecting workers in hazardous environments. From fire extinguishers for incipient fire response to mobile and fixed fire suppression solutions, our solutions provide reliable hazard protection across multiple mining operations. Paired with preventive tools that reduce combustible dust, we help mining facilities maintain safer conditions and stronger overall fire protection.

We’ll help your mining company find the right fire protection equipment and strategies for safer, more efficient operations.


 | Today Visitors | 121 |
 | Total Visitors | 338774 |
 | Online Visitors | 14 |

Address: 72 Nguyen Trai ,Thanh Xuan District, Ha Noi
Telephone: 091 352 7238 | Fax: 091 352 7238
Email: f500hct@gmail.com ; cnccompany2000@gmail.com
© 2026, CNC Equipment Company Limited. All rights reserved.